Product Overview
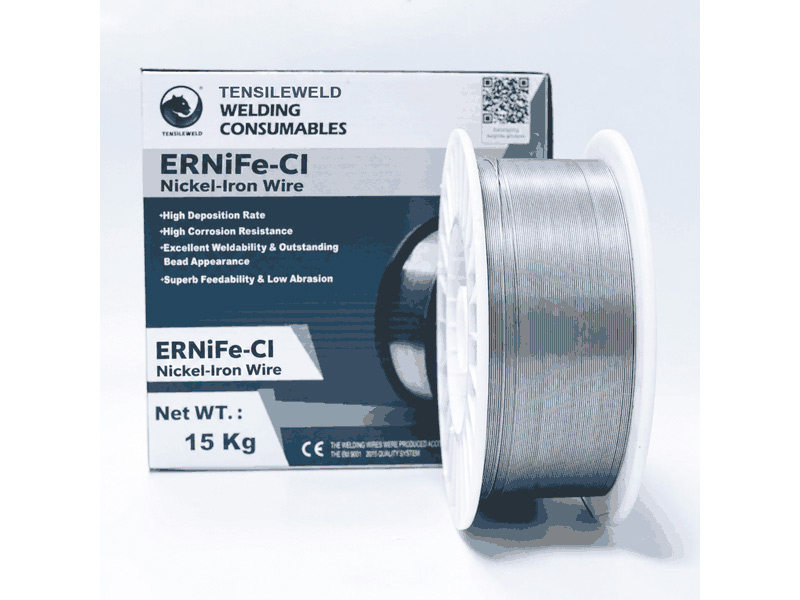
Grade:NiFe-1 Nickel‑Iron Wire
NiFe-1 nickel‑iron alloy solid MIG welding wire is a well‑balanced performance cast‑iron repair consumable. It features high weld strength and excellent toughness together with good impact‑resistance. It offers a nice balance between cost and welding performance. Weld deposit has good machinability. This wire is specially suitable for ductile iron and heavy‑section thick cast‑iron repair work.
Chemical Composition (Wt%)
| Element | Content |
|---|---|
| Ni | 45 – 75 |
| Fe | Balance |
| C | ≤ 2.0 |
| Si | ≤ 4.0 |
| Mn | ≤ 2.5 |
| S | ≤ 0.03% |
| P | ≤ 0.03% |
| Other | ≤ 1.0% |
Mechanical Properties (Weld Deposit)
| Item | Result |
|---|---|
| Tensile Strength | ≥470 MPa |
| Elongation | ≥13 % |
Recommended Welding Parameters
| Parameter | Value |
|---|---|
| Welding Current | 100‑140 A |
| Arc Voltage | 19‑23 V |
| Shielding Gas | Pure Argon / Argon +5~10% CO₂ |
| Wire Feed Speed | 4.5‑6.5 m/min |
Features & Characteristics
High weld strength and excellent toughness
Good impact‑resistance performance
Balanced cost‑to‑performance ratio
Satisfactory post‑weld machinability
Ideal choice for ductile iron and thick heavy cast‑iron workpieces
Typical Application
Engine cylinder blocks
Pump housings, compressor shells
Heavy‑equipment bases, gearbox castings
Repair work for heavy‑load grey cast iron and ductile iron components
Welding Operation Guidelines
1.Grind out cracks and prepare an open V‑groove to guarantee full penetration.
2.Avoid long continuous welding runs.
3.Strictly control inter‑pass temperature below 250 °C.
4.Preheat thick workpieces to 100‑300 °C before welding.
5.Hammer each weld bead after completion to relieve internal residual stress.