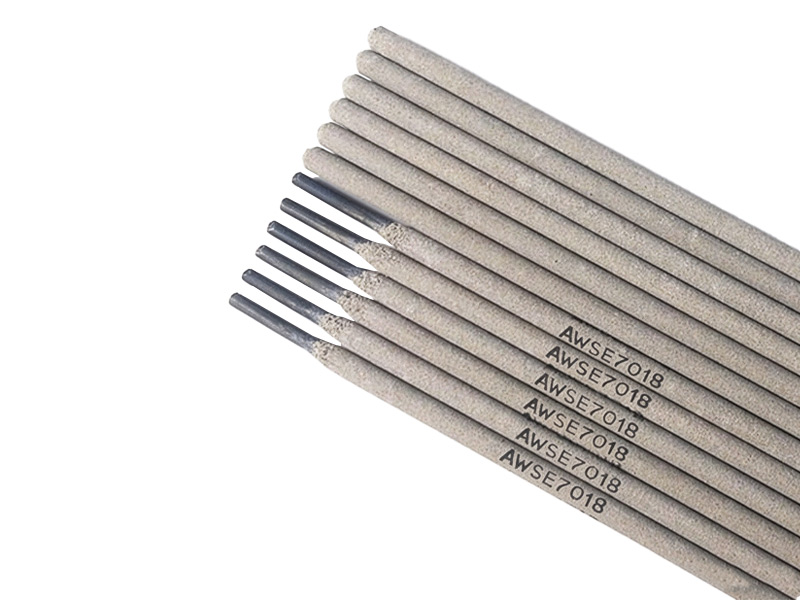
E7018 is an outstanding quality welding electrode covered with extra low hydrogen potassium type coating for high tensile strength mild steels and low alloy steels.
BS EN IS0 2560-B-E 49 18-1 A
CSA W48-06 E4918-1 H8
JIS Z3212D5016
GB/T5117E5018-1
Type of Covering: Extra Low Hydrogen, Potassium, Iron Powder
Welding Position: F,H,HF,OH,V
Type of Current: AC or DCEP
Features & Applications
E7018 is an outstanding quality welding electrode covered with extra low hydrogen potassium type coating for high tensile strength mild steels and low alloy steels. Its nominal welding efficiency is about 110% due to iron powder is contained. The weld metal shows an excellent low temperature toughness and high crack-resistance. It is widely used in important projects of ships, boilers, high pressure vessels, bridges,skyscrapers, offshore drilling platforms, nuclear power plants and so on.
Chemical Composition of Deposited Metal(%)
| C | Mn* | Si | S | P | Ni* | Cr* | Mo* | V* | |
| Standard | ≤0.15 | ≤1.60 | ≤0.75 | ≤0.035 | ≤0.035 | ≤0.30 | ≤0.20 | ≤0.30 | ≤0.08 |
| Typical | 0.068 | 1.36 | 0.51 | 0.010 | 0.016 | 0.006 | 0.027 | 0.003 | 0.016 |
The total amount of element with * ones should be≤1.75%
Mechanical Properties of Deposited Metal(AW)
| Yield PointReh (Mpa) |
Tensile StrengthRm (Mpa) |
Elongation A4 (%) |
Impact Value(J) | |||
| -20°C | -30°C | -46°C | ||||
| Standard | ≥375 | 490-660 | ≥22 | ≥47 | ≥27 | ≥27 |
| Typical | 440 | 540 | 30 | 170 | 150 | 130 |
The standard of mechanical properties conforms to shipping institutions and the certificate of inspection would follow it unless the purchaser has special requirement.
Diffusible hydrogen in deposited metal: ≤5 ml /100 g(mercury process)
X-ray radiographic inspection: Grade Ⅰ
Size & Recommended Current(AC≥70V or DC⁺)
| Size(mm) | 2.5×300 | 2.5×350 | 3.2×350 | 3.2×450 | 4.0×400 | 4.0×450 | 5.0×400 | 5.0×450 | |
| Piece(5kg) | ≈290 | ≈248 | ≈145 | ≈114 | ≈84 | ≈75 | ≈51 | ≈45 | |
| Current(A) | F,H | 70-100 | 70-100 | 100-140 | 100-140 | 140-170 | 140-170 | 190-240 | 190-240 |
| V,OH | 60-70 | 60-70 | 80-110 | 80-110 | 130-150 | 130-150 | — | — | |
Notice: 1. The rod should be baked at 400°C for 1-2 hours before use.
2. The surfaces to be welded must be cleaned away impurities of oil contamination, rust, moisture and so on.
3. Short arc and narrow-gap welding is recommended.
Position Welding