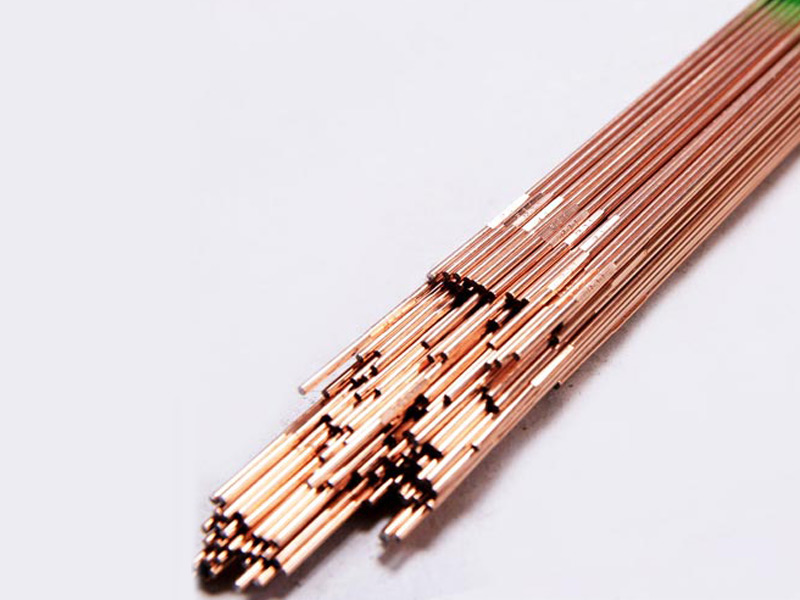
TIG Steel Alloy Welding Wire ER80S-B2,TIG Steel Alloy Welding Rod ER80S-B2,Steel Alloy Welding Rod ER80S-B2,Steel Alloy Welding Wire ER80S-B2,ER80S-B2.
AWS A5.28 ER80S-B2
BS EN IS0 21952-A-W CrMo1Si
JIS Z3316 YGT1CM
Welding Position: F,H,HF,OH,V
Type of Current: DCEP
Features & Applications
ER80S-B2 is suitable for structures fabricated by 1.25Cr-0.5Mo series pearlitic heat-resisting low alloy steels such as high press steam pipes of boiler or steam turbine which work temperature is lower than 510℃.
Chemical Composition of the Wire(%)
| C | Mn | Si | S | P | Ni | Cr | Mo | V | Cu | |
| Standard | 0.06-0.15 | 1.00-1.45 | 0.60-1.05 | ≤0.035 | ≤0.025 | — | ≤1.55 | ≤0.15 | — | ≤0.50 |
| Typical | 0.076 | 1.22 | 0.69 | 0.010 | 0.012 | — | 1.21 | 0.050 | — | 0.13 |
Mechanical Properties of Deposited Metal(AW)
| Yield Point Reh (Mpa) |
Tensile Strength Rm(Mpa) |
Elongation A4(%) |
Impact Value(J) | Shield Gas | |
| 25°C | CO₂ 20%CO2+80%Ar |
||||
| Standard | ≥505 | ≥610 | ≥21 | ≥90 | |
| Typical | 545 | 640 | 29 | 132 |
The standard of mechanical properties conforms to shipping institutions and the certificate of inspection would follow it unless the purchaser has special requirement.
Size & Recommended Current(DC⁺)
| Diameter(mm) | 0.6 | 0.8 | 0.9 | 1.0 | 1.2 | 1.6 |
| Current(A) | 60-120 | 40-150 | 40-180 | 50-220 | 80-350 | 120-550 |
Notice:
1. To avoid rust the wire must be kept in dry condition and keep the package in good condition also before welding
2. To avoid welding defect the shield gas should be pure particularly no moisture in it.
3. The surfaces to be welded must be cleaned away impurities of oil contamination, rust, moisture and so on.
4. The welding conditions mentioned above for reference only and it is better to do a welding procedure qualification according to project before put it into formal welding.