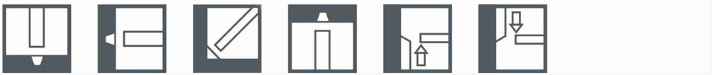
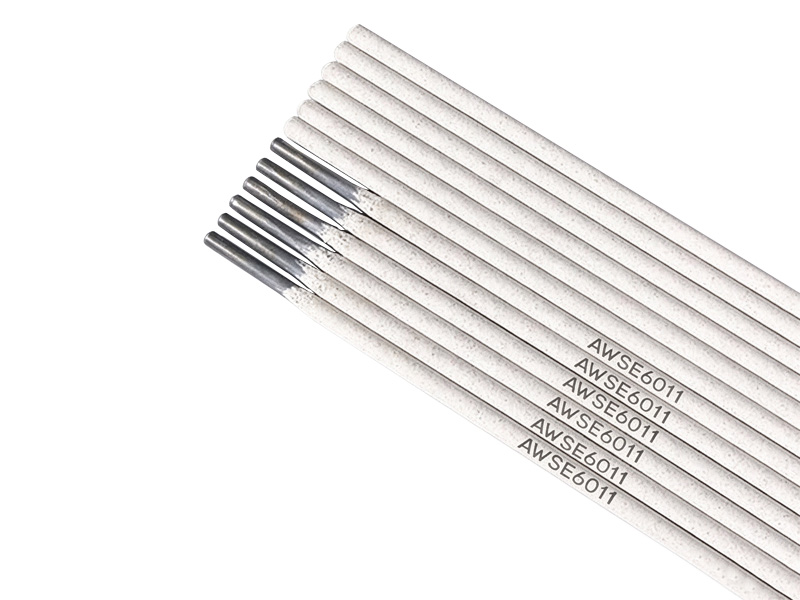
E6011 is suitable for butt welding, corner joint welding and lap welding for sheet steels.
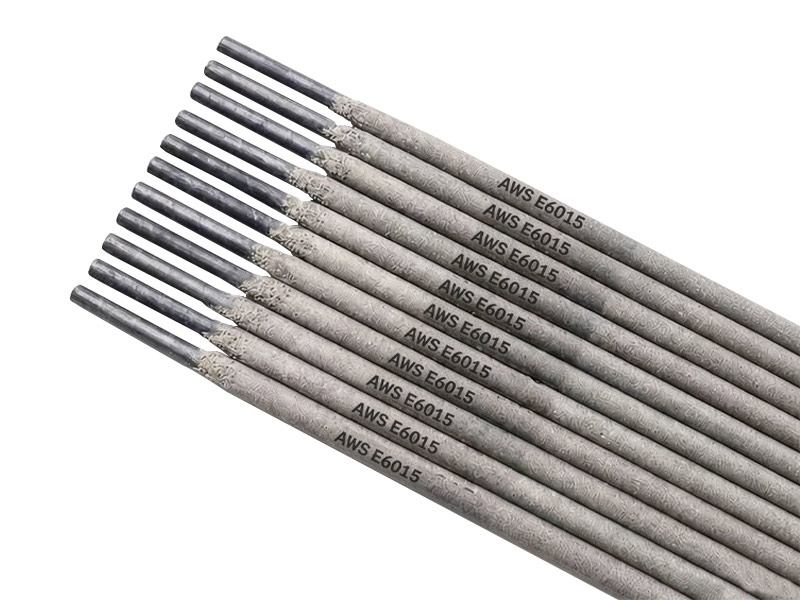
AWS A5.1 E6011
BS EN IS02560-B-E4311 A
CSA W48-01 E4311
JIS Z3211 D4311
GB/T5117 E4311
Type of Covering: High Cellulose, Potassium
Welding Position: F,H,HF,OH,V,VD
Type of Current: AC or DCEP
Features & Applications
E6011 is suitable for butt welding, corner joint welding and lap welding for sheet steels, such as structures of powder plant’s flue and air duct, oil tank of transformer upper structures of hull, vehicle plate and so on. The welding rod is unfavourable to weave too wide and the length of voltaic arc should be appropriate. It is not suitable for multi-layer welding and not for cosmetic welding.
Use environmentally friendly cellulose as material to produce E6011 , that no odour and lower smoke.Stable arc with high arc force brings excellent weld ability in all position including vertical down operation.
Chemical Composition of Deposited Metal(%)
| C | Mn | Si | S | P | Ni | Cr | Mo | V | |
| Standard | ≤0.20 | ≤1.20 | ≤1.00 | —- | —- | ≤0.30 | ≤0.20 | ≤0.30 | ≤0.08 |
| Typical | 0.096 | 0.68 | 0.2 | 0.017 | 0.018 | 0.008 | 0.041 | 0.001 | 0.012 |
Mechanical Properties of Deposited Metal(AW)
| Yield Point Reh (Mpa) | Tensile Strength Rm(Mpa) | Elongation A4(%) | Impact Value(J) | |
| -30°C | ||||
| Standard | ≥330 | ≥430 | ≥22 | ≥27 |
| Typical | 405 | 500 | 30 | 75 |
X-ray radiographic inspection: Grade II
Size,Piece & Recommended Current(AC or DC⁺)
| Size(mm) | 2.5×300 | 3.2×350 | 4.0×350 | 5.0×350 | |
| Piece(5kg) | ≈328 | ≈185 | ≈120 | ≈76 | |
| Current(A) | F,H | 30-50 | 70-100 | 90-140 | 150-200 |
Notice: 1. Good condition of packaging and storage for it is important.
2. Normally it does not need re-dry.When it is damped seriously re-baked at temperature of 70°C-80°C for 30-60 minutes before welding.
3. To increase performance of welding, when using Dia. 5.Omm one, bigger thrust and smaller current are recommended.
Welding Position