Product Description
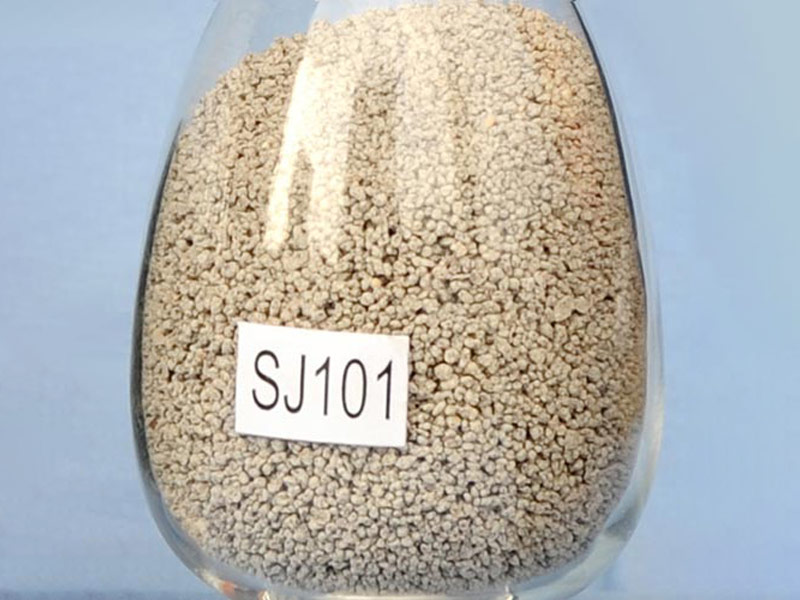
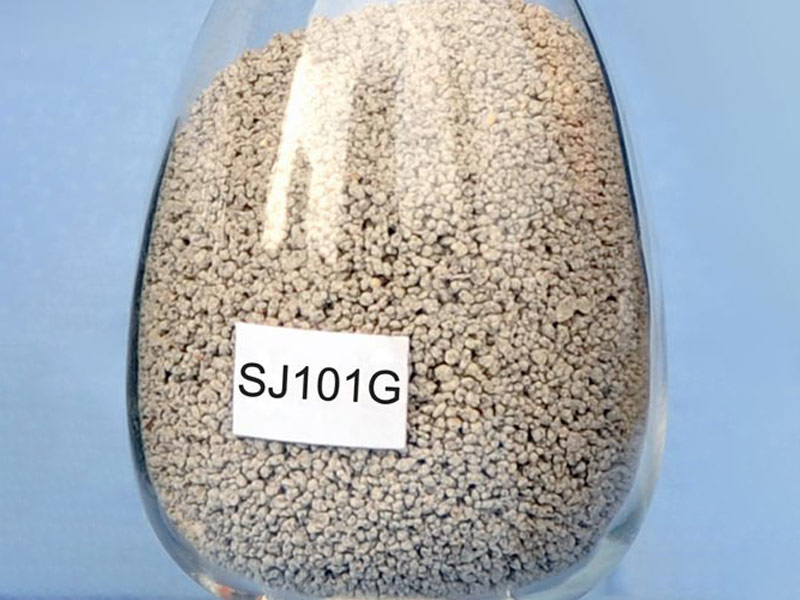
Submerged Arc Welding Flux sj101G
SJ101G
Specification: EN760 SAFB 155 AC H5
AWS A.5.17/5.23 F7A2-EM12K F7A4-EH14 F7A6-EG-G F8A2-EA2-A2
Applications:
Single and multi-layer welding of steel for low temperature service used in offshore structures, chemical vessels, APl pipes, windmils and low temperature service equipments.
Characteristics: SJ101Gis an agglomerated fluoride-basic type flux
Metallurgical behavior:
The behavior of silicon and manganese is neutral, so it is better to weld with wires containing relatively high manganese and silicon.
Basicity: 3.1(BIIW)
Damp flux should be re-dried at 300- 350 °C for 2 hours. Rust, grease and moisture on the weldment should be removed before welding.
Chemical Composition of SJ101G (%)
| Si0₂+Ti0₂ | CaF₂ | Al₂0₃+Mn0 | CaO+MgO | S | P |
| 18-25 | 16-25 | 23-30 | 28-35 | ≤0.06 | ≤0.08 |
Mechanical Properties of the All-Weld
| Wire | Yield Point σₛ (Mpa) | Tensile Strength σᵦ(Mpa) | Elongation σ₅(%) | Charpy V Notch Impact Value(J) | ||
| -20°C | -40°C | -50°C | ||||
| EM12K | ≥400 | 490-600 | ≥22 | ≥60 | — | — |
| EH14 | ≥420 | 510-600 | ≥22 | ≥70 | ≥57 | ≥27 |
| EG | ≥430 | 530-690 | ≥22 | ≥90 | ≥80 | ≥42 |
| EA2 | ≥500 | 600-700 | ≥20 | ≥60 | ≥55 | ≥34 |