Product Description
Manganese Steel & High-Chromium Hardfacing Flux-Cored Welding Wires (TW614–TW765 Series) — combines work-hardening austenitic manganese steel wires (TW614–TW641) for extreme impact with ultra-hard complex chromium/niobium/vanadium/boron carbide open-arc wires (TW740–TW765, 59–67 HRC) for severe mineral abrasion.
Product core positioning: Dual-purpose mining & cement hardfacing FCW family: work-hardening Mn steel (up to 450 HB after impact) and complex carbide overlays (up to 67 HRC).
Chemical Composition (wt%) & Hardness (TW614–TW765 Series)
| Product | C | Si | Mn | Cr | Ni | Fe | Others | Hardness |
|---|---|---|---|---|---|---|---|---|
| TW614-O / TW614-S | 0.90 | 0.50 | 14.00 | 0.50 | 0.50 | Bal. | — | 175–225 HB (after impact: 450 HB) |
| TW618-O / TW618-S | 0.90 | 0.60 | 15.00 | 3.50 | 3.50 | Bal. | — | 180–220 HB (after impact: 450 HB) |
| TW618TiC-O | 1.30 | 0.50 | 12.00 | 3.00 | — | Bal. | Ti: 3.10 | 38–42 HRC |
| TW619-O / TW619-S | 1.10 | 0.70 | 19.50 | 5.00 | — | Bal. | — | 180–230 HB (after impact: 450 HB) |
| TW624L-S | 0.04 | 0.30 | 18.50 | 3.65 | — | Bal. | Nb: 2.60, Mo: 0.80, Ti: 0.12 | 180–220 HB |
| TW624-O / TW624-S | 1.00 | 0.43 | 17.50 | 8.50 | — | Bal. | Nb: 2.50, Ti: 0.10 | 230–270 HB / 300–350 HB |
| TW641-O (AP-O) / TW641-G | 0.38 | 0.35 | 16.50 | 12.50 | — | Bal. | — | 180–210 HB |
| TW740-O (101HD) | 6.50 | 1.00 | 2.50 | 29.50 | — | Bal. | — | 59–62 HRC |
| TW740Mo-O (100HC) | 4.50 | 1.50 | 1.50 | 25.50 | — | Bal. | Mo: 1.20 | 60–62 HRC |
| TW740MoZr-O (CP-2000) | 5.00 | 1.20 | 1.50 | 25.00 | — | Bal. | Mo: 1.10, Zr: 0.45 | 60–64 HRC |
| TW741B-O | 5.20 | 1.26 | 2.70 | 26.70 | — | Bal. | Nb: 1.88, B: 0.58 | 60–63 HRC |
| TW742-O (CP-2001) | 4.60 | 1.10 | 1.30 | 24.50 | — | Bal. | Mo: 3.00, Nb: 1.10, V: 2.00 | 63–67 HRC |
| TW742B-O | 5.25 | 1.15 | 2.30 | 24.65 | — | Bal. | Nb: 3.99, B: 0.78 | 61–64 HRC |
| TW743-O (A43-O, 143) | 5.60 | 1.30 | 0.50 | 21.50 | — | Bal. | Nb: 6.75 | 63–65 HRC |
| TW743B-O | 5.20 | 1.10 | 0.60 | 21.50 | — | Bal. | Nb: 6.75, B: 1.00 | 63–65 HRC |
| TW744B-O | 5.30 | 1.05 | 1.00 | 24.50 | — | Bal. | Nb: 1.50, Mo: 3.25, B: 0.50, Ti: 0.55, Zr: 0.50, V: 2.00 | 64–66 HRC |
| TW745-O (A4-O, 145) | 5.50 | 0.75 | 1.00 | 21.00 | — | Bal. | Nb: 6.00, Mo: 6.30, V: 1.00, W: 1.90 | 64–65 HRC |
| TW765-O (A65-O) | 4.70 | 1.00 | 0.50 | 12.50 | — | Bal. | Nb: 5.70, Co: 7.80, V: 5.50 | 65–67 HRC |
Core Advantages & Features
- Manganese steel grades work-harden rapidly under heavy impact (from ~180 HB to 450 HB) without cracking.
- Complex carbide open-arc grades (TW740–TW765) form dense Cr/Nb/V/Mo/B carbides up to 67 HRC for extreme abrasion.
- Self-shielded open-arc (-O) operation ideal for field repair and automated wear-plate cladding.
Typical Application Fields
- Jaw crushers, cone crushers, hammer mills, and railway frogs (Mn series)
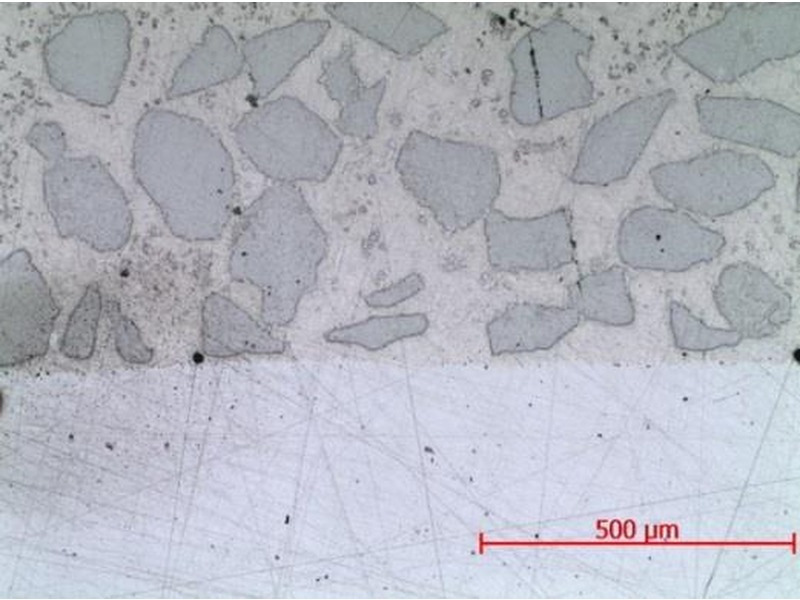
- Bimetallic chromium carbide overlay (CCO) wear plates
- Cement vertical mills, coal chutes, sinter crushers, and blast furnace bells