Product Description
Laser Cladding Powder TWDNi0103B (NiCrBSi + 57% WC Composite Powder) — is a high-purity NiCrBSi + Tungsten Carbide (57.0–57.6% WC) composite laser cladding powder engineered for extreme abrasive wear resistance, high coating density, low oxygen (<0.08%), and crack-free metallurgical bonding.
Product core positioning: Flagship NiCrBSi + WC composite laser cladding powder featuring 55–60 HRC hardness and verified ASTM G65 wear loss of just 0.20 g / 30 min.
1. Chemical Analysis (wt%)
| Element | Wt.% | Element | Wt.% |
|---|---|---|---|
| Total Carbon (Ct) | 2.4–2.9 | Oxygen (O) | <0.08 |
| Chromium (Cr) | 6.0–8.1 | Cobalt (Co) | <0.06 |
| Boron (B) | 1.2–1.8 | Silicon (Si) | 1.4–2.2 |
| Iron (Fe) | ≤3.0 | Nickel (Ni) | Bal. |
| Tungsten Carbide (WC) | 57.0–57.6 | Other Metallic Impurities | ≤1.0 |
2. Physical Properties & 3. ASTM G65 Wear-Resistant Testing
| Flowability (s/50g) | Apparent Density (g/cm³) | Hardness (HRC) | ASTM G65 Wear Loss |
|---|---|---|---|
| 12.0–15.0 | 4.70–5.90 | 55–60 | 0.20 g / 30 min |
4. Screen Analysis (ASTM-B214)
| Size Fraction | Min Wt.% | Max Wt.% |
|---|---|---|
| +150 µm | — | 5.0 |
| -150 / +120 µm | — | — |
| -120 / +106 µm | — | — |
| -106 / +75 µm | — | — |
| -75 / +53 µm | — | — |
| -53 µm | — | 5.0 |
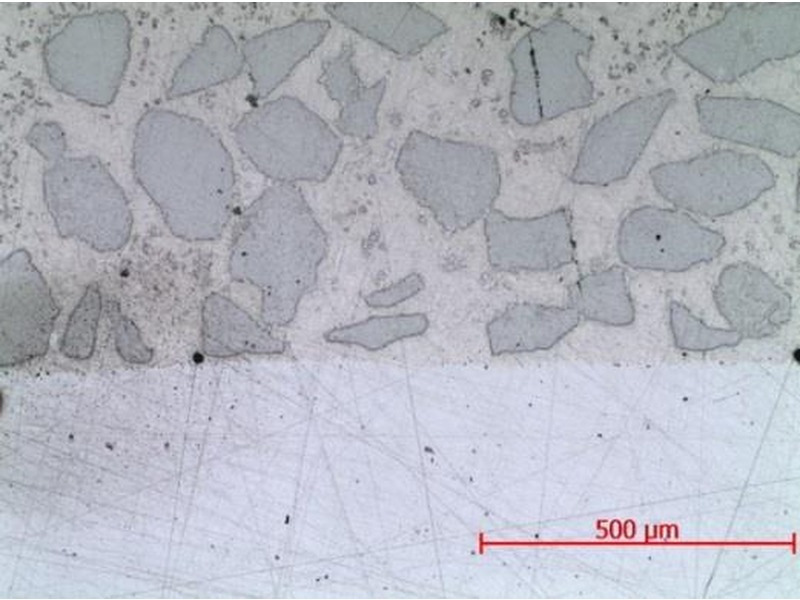
5. Metallographical Structure
Core Advantages & Features
- Ultra-low oxygen content (<0.08%) produces dense, pore-free, crack-free laser cladding layers.
- Excellent powder flowability (12.0–15.0 s/50g) ensures smooth, steady feeding in coaxial laser cladding heads.
- Proven extreme wear performance: 55–60 HRC coating with ASTM G65 wear loss of only 0.20 g / 30 min.
Typical Application Fields
- Oil & gas downhole stabilizers, mud motor rotors, and drilling sleeves
- Coal mining hydraulic props, shearer picks, and scraper conveyors
- Extruder screws, agricultural wear parts, and heavy mineral processing components