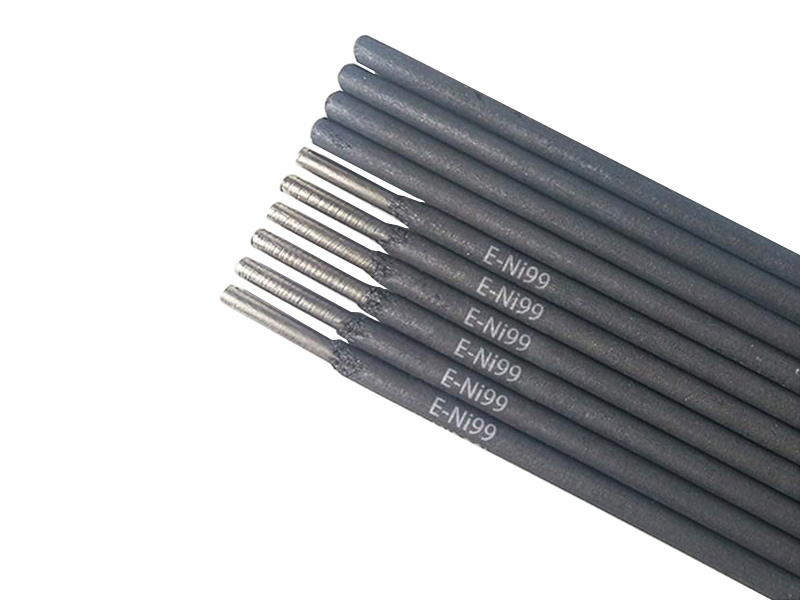
Pure Nichel Core Covered Welding Rod ENi-CI
AWS A5.15 ENi-Ci
IS0 1071-E C Ni-Ci
JIS Z3252 DFCNi
GB/T 10044 EZNi-1
Type of Covering: Graphitemould
Welding Position: F,H,HF,OH,V
Type of Current: AC or DCEP
Features & Applications
ENi-Ci is the best for repair welding cracked or worn castings of grey cast iron, such as covers of cylinders, gear cases of engine seating and guideways of machine tools and so on. Also it is joining cast iron parts with dissimilar metals or surfacing welding. Color of the coating is dark black. The welding performance is very good and the machinability of the deposited metal is good.
Chemical Composition of Deposited Metal(%) – ENi-Ci
| C | Mn | Si | S | Ni | Al | Cu | Fe | Others | |
| Standard | ≤2.00 | ≤2.50 | ≤4.00 | ≤0.03 | ≥85 | ≤1.00 | ≤2.50 | ≤8.0 | ≤1.00 |
| Typical | 0.590 | 0.07 | 1.5 | 0.004 | 94.00 | 0.032 | 0.002 | 0.021 | 0.14 |
Size,Piece & Recommended Current(AC or DC )
| Size(mm) | 2.5×300 | 3.2×350 | 4.0×350 | 5.0×350 | |
| Piece(1kg) | ≈51 | ≈31 | ≈21 | ≈14 | |
| Current(A) | 60-90 | 90-110 | 120-150 | 150-180 | |
Notice:
1. The rod should be baked at 80″C -120″C for 1 hours before use.
2. The surfaces to be welded must be cleaned away impurities of oil contamination, rust, moisture and so on.
3. When welding, hammering the weld joint to dispel stress around the welding region to avoid crack.
4. To increase ability of crack-resisting and machinable, small current is recommended, meanwhile could reduce impurities to permeate the weld seam from base metal.