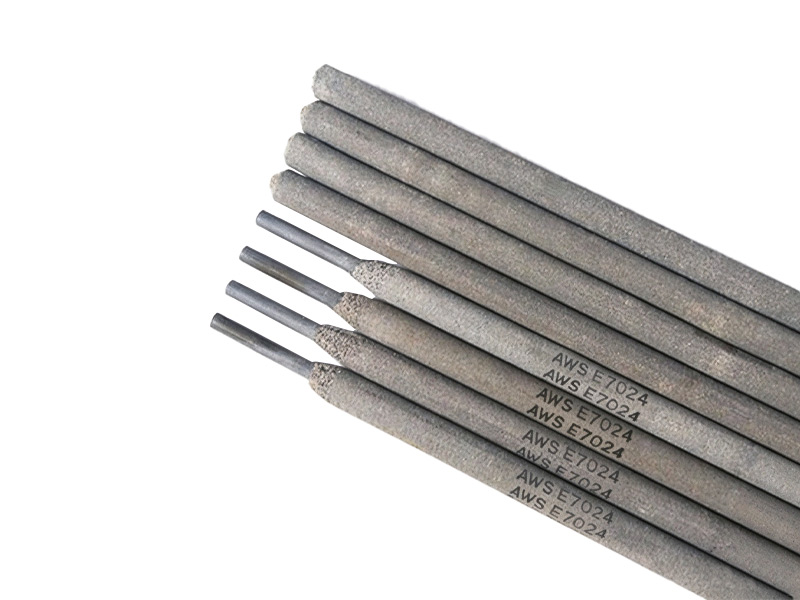
Product Description
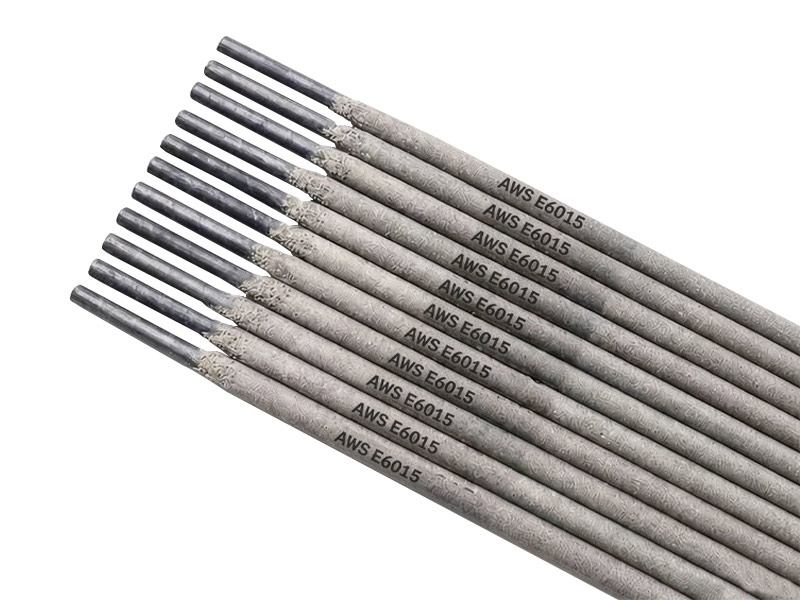
E7024 is the high tensile strength steel welding electrode. It used for flat and horizontal fillet welding ship structures, H beams of bridges.
AWS A5.1 E7024
BS EN IS02560-B-E 49 24A
CSA W48-06 E4924
JIS Z3212 D5024
GB/T 5117E5024
Type of Covering: Iron powder, Titania
Nelding Position: F,H,HF
fype of Current: AC or DCEP
Features & Applications
E7024 is the high tensile strength steel welding electrode. It used for flat and horizontal fillet welding ship structures, H beams of bridges, as well as general steel structures.
Chemical Composition of Deposited Metal(%)
| C | Mn | Si | S | P | Ni | Cr | Mo | V | |
| Standard | ≤0.15 | ≤1.25 | ≤0.90 | ≤0.035 | ≤0.035 | ≤0.30 | ≤0.20 | ≤0.30 | ≤0.08 |
| Typical | 0.069 | 0.82 | 0.46 | 0.016 | 0.022 | 0.005 | 0.026 | 0.003 | 0.016 |
Mechanical Properties of Deposited Metal(AW)
| Yield PointReh (Mpa) | Tensile StrengthRm (Mpa) | Elongation A4(%) | Impact Value(J) | |
| 0°C | ||||
| Standard | ≥375 | 490-660 | ≥22 | ≥47 |
| Typical | 450 | 520 | 29 | 75 |
X-ray radiographic inspection: Gradel
Size & Recommended Current(AC or DCt)
| Size(mm) | 2.5×300 | 3.2×350 | 4×400 | 5×400 | |
| Current(A) | F,H | 70-110 | 100-140 | 140-180 | 180-230 |
| V,OH | 50-80 | 80-110 | 130-170 | – | |
Notice:
1. The rod should be baked at 350°C for 1 hour before use.
2. The surfaces to be welded must be cleaned away impurities of oil contamination, rust, moisture and so on.
3. Short arc and narrow-gap welding is recommended
All Position Welding