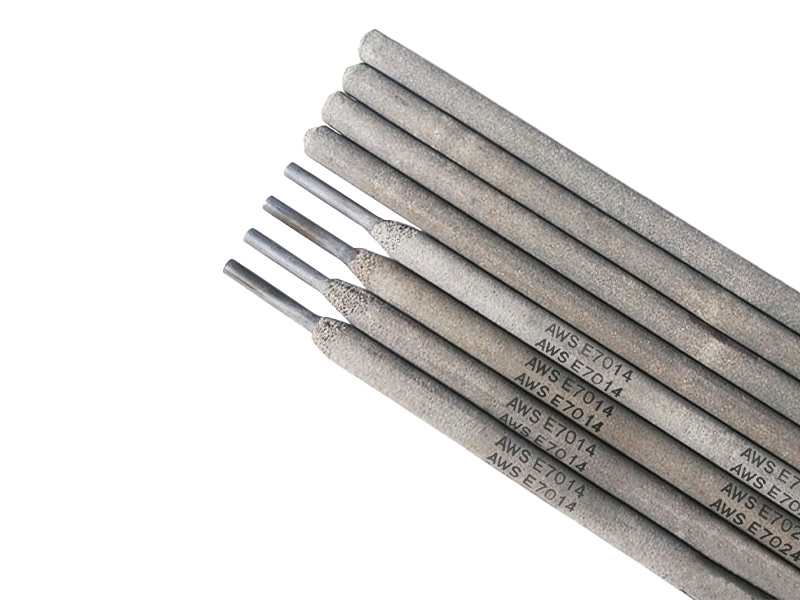
Product Description
E7014 nominal deposited efficiency is about 110% and it is used for welding structures fabricated by equivalent tensile strength mild steels or low alloy steels.
AWS A5.1 E7014
BS EN IS0 2560-B-E 49 14 A
CSAW48-06 E4914
JIS Z3212 D5014
GB/T 5117E5014
Type of Covering: Iron powder, Titania
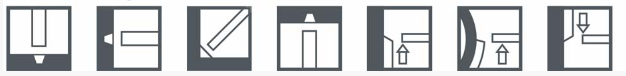
Welding Position: F,H,HF,OH,V
Type of Current: AC or DCEP or DCEN
Features & Applications
E7014 nominal deposited efficiency is about 110% and it is used for welding structures fabricated by equivalent tensile strength mild steels or low alloy steels, such as machineries, vehicles and so on.
Chemical Composition of Deposited Metal(%)
| C | Mn* | Si | S | P | Ni* | Cr* | Mo* | V* | |
| Standard | —- | ≤1.25 | ≤0.90 | ≤0.035 | ≤0.035 | ≤0.30 | ≤0.20 | ≤0.30 | ≤0.08 |
| Typical | 0.068 | 0.65 | 0.42 | 0.027 | 0.025 | 0.011 | 0.006 | 0.013 | 0.06 |
Mechanical Properties of Deposited Metal(AW)
| Yield PointReh (Mpa) | Tensile StrengthRm (Mpa) | Elongation A4(%) | |
| Standard | ≥375 | 490-660 | ≥22 |
| Typical | 450 | 550 | 30 |
X-ray radiographic inspection: Grade II
Size & Recommended Current(AC or DC⁺)
| Size(mm) | 2.5×300 | 3.2×300 | 4×400 | 5.0×400 | |
| Current(A) | F,H | 60-90 | 80-120 | 140-180 | 180-230 |
| V,OH | 50-80 | 70-110 | 130-170 | – | |
Notice: Normally the rod does not need to re-dry in case it is affected with damp seriously re-bake it as 150°C for 30-60 minutes before use
All Position Welding