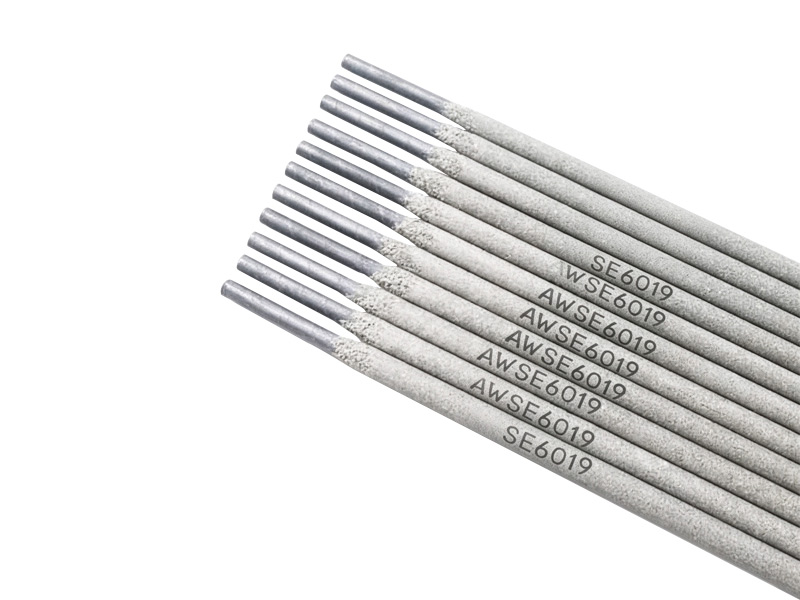
Product Description
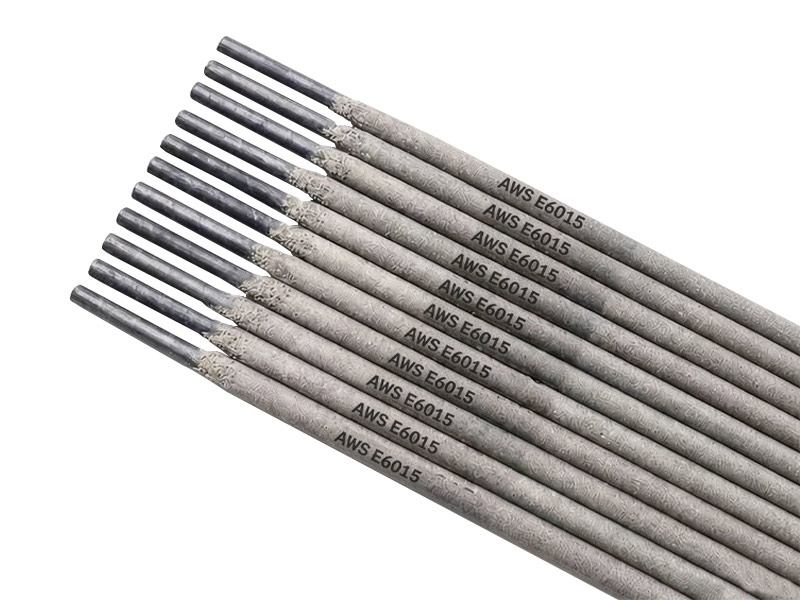
WELDING ELECTRODE E6019
AWS A5.1 E6019
BS EN IS0 2560-B-E 43 19 A
CSA W48-01 E4319
JIS Z3211 D4319
GB/T5117 E4319
Type of Covering: Titania, Potassium, Iron Oxide
Welding Position: F,H,HF,OH,V
Type of Current: AC, DCEP or DCEN
Features & Applications
E6019 is suitable for welding ship hulls, pressure vessels, bridges as well as structural fabrications.
Chemical Composition of Deposited Metal(%)
| C | Mn | Si | S | P | Ni | Cr | Mo | V | |
| Standard | ≤0.20 | ≤1.20 | ≤1.00 | ≤0.035 | ≤0.040 | ≤0.30 | ≤0.20 | ≤0.30 | ≤0.08 |
| Typical | 0.095 | 0.52 | 0.27 | 0.018 | 0.026 | 0.052 | 0.057 | 0.004 | 0.014 |
Mechanical Properties of Deposited Metal(AW)
| Yield Point Reh (Mpa) | Tensile Strength Rm(Mpa) | Elongation A4(%) | Impact Value(J) | |
| 0°C | ||||
| Standard | ReH≥306 | 400-560 | ≥22 | ≥47 |
| Typical | 395 | 480 | 28 | 59 |
X-ray radiographic inspection: Grade I
Size,Piece & Recommended Current(AC or DC⁺)
| Size(mm) | 2.5×300 | 3.2×350 | 4.0×400 | 5.0×450 | |
| Piece(5kg) | ≈292 | ≈156 | ≈89 | ≈48 | |
| Current(A) | F,H | 90-120 | 100-150 | 140-210 | 190-260 |
| OH,H | 70-100 | 90-120 | 140-170 | — | |
Notice: 1. Good condition of packaging and storage for it is important.
2. Normally it does not need re-dry. When it is damped seriously re-baked at temperature of 70 C-80°C for 30-60 minutes before welding.