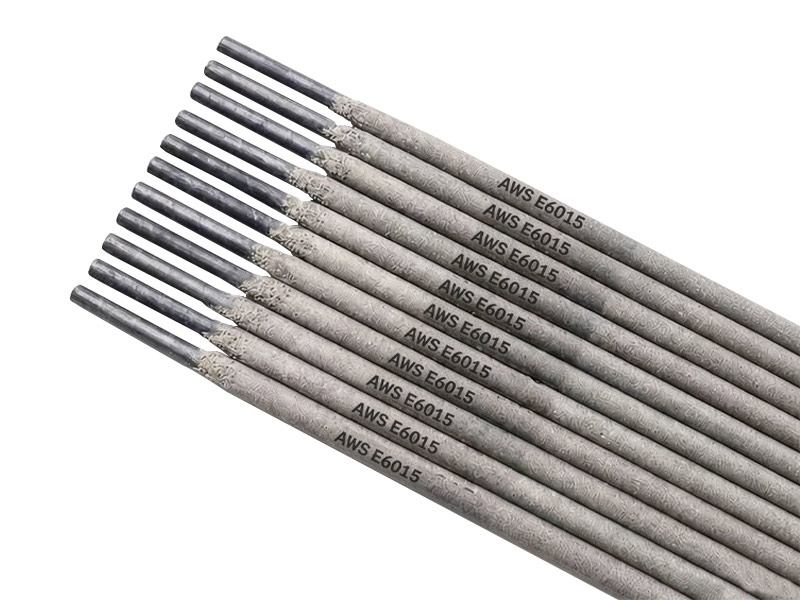
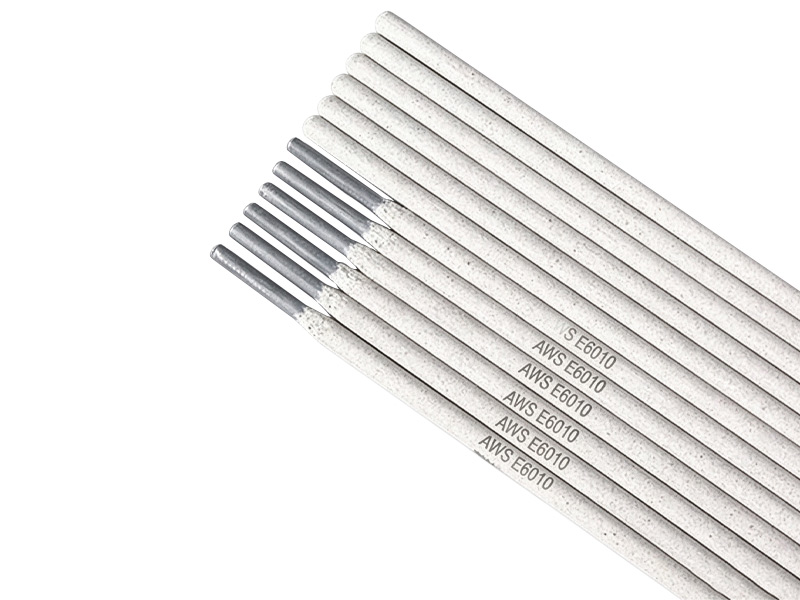
E6010 is mainly used for backing welding of substrate, root passes, filler and cosmetic welding of mild steel pipes.
AWS A5.1 E6010
BS EN ISO 2560-B-E 43 10 A
CSA W48-01 E4310
GB/T 5117 E4310
Type of Covering: High Cellulose, Sodium
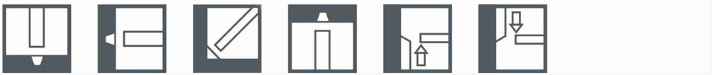
Welding Position: F,H,HF,OH,V,VD
Type of Current: D C E P
Features & Applications
E6010 is mainly used for backing welding of substrate, root passes, filer and cosmetic welding of mild steel pipes. It could be fashioned by one-side welding with back formation.
Use environmentally friendly cellulose as material to produce E6010,that no odour and lower smoke.Stable arc with high arc force brings excellent weld ability in all position including vertical down operation.
Chemical Composition of Deposited Metal(%)
| C | Mn | Si | S | P | Ni | Cr | Mo | V | |
| Standard | ≤0.20 | ≤1.20 | ≤1.00 | —- | —- | ≤0.30 | ≤0.20 | ≤0.30 | ≤0.08 |
| Typical | 0.091 | 0.55 | 0.17 | 0.010 | 0.011 | 0.011 | 0.022 | 0.001 | 0.012 |
Mechanical Properties of Deposited Metal(AW)
| Yield Point Reh (Mpa) | Tensile Strength Rm(Mpa) | Elongation A4(%) | Impact Value(J) | |
| -30°C | ||||
| Standard | ≥330 | ≥430 | ≥22 | ≥27 |
| Typical | 400 | 500 | 29 | 80 |
X-ray radiographic inspection: Grade II
Size,Piece & Recommended Current(DC⁺)
| Size(mm) | 2.5×300 | 3.2×350 | 4.0×350 | 5.0×350 | |
| Piece(5kg) | ≈328 | ≈185 | ≈120 | ≈76 | |
| Current(A) | F,H | 60-90 | 70-110 | 110-150 | 150-200 |
| OH,VD | 50-80 | 60-100 | 100-140 | 140-180 | |
Notice: 1. Good condition of packaging and storage for it is important.
2. Normally it does not need re-dry.When it is damped seriously re-baked at temperature of 70°C-80°C for 30-60 minutes before welding.
3. To increase performance of welding, when using Dia. 5.Omm one, bigger thrust and smaller current are recommended.
Welding Position