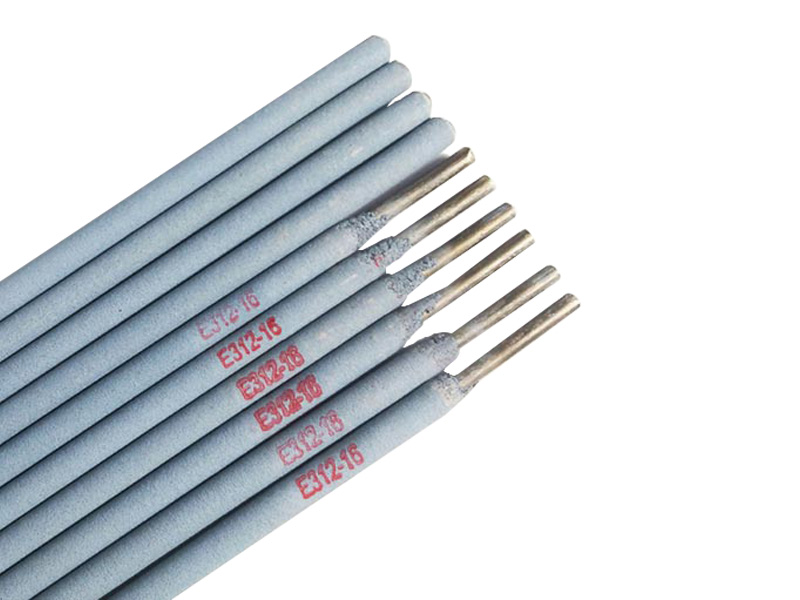
Stainless Steel Electrode E312-16
AWS A5.4 E312-16
IS0 3581-B-ES312-16
BS EN 1600-E 29 9 R32
CSA W48 E312-16
JIS Z3221 D312-16
GB/T983 E312-16
Type of Covering: Lime-titania
Welding Position: F,H,HF,OH,V
Type of Current: AC or DCEP
Features & Applications
E312-16 deposits a ferritic-austenitic duplex weld metal with around 40% ferrite so it has excellent crack resistance. It is suitable for welding Cr29Ni9 cast steels, high carbon steels, tool steels, problem steels as well as for dissimilar steel welding.
Chemical Composition of Deposited Metal(%)
| C | Mn | Si | Cr | Ni | Mo | Cu | S | P | |
| Standard | ≤0.15 | 0.50-2.50 | ≤1.00 | 28.0-32.0 | 8.0-10.5 | ≤0.75 | ≤0.75 | ≤0.03 | ≤0.04 |
| Typical | 0.085 | 1.11 | 0.78 | 29.39 | 9.97 | 0.16 | 0.20 | 0.011 | 0.028 |
Mechanical Properties of Deposited Metal(AW)
| Tensile Strength Rm(Mpa) | Elongation A4(%) | |
| Standard | ≥660 | ≥22 |
| Typical | 785 | 26 |
Size,Piece & Recommended Current(AC or DC⁺)
| Size(mm) | 2.0×300 | 2.5×300 | 3.2×350 | 4.0×400 | 5.0×400 | |
| Piece(5kg) | ≈400 | ≈300 | ≈132 | ≈77 | ≈53 | |
| Current(A) | F,H | 30-50 | 50-85 | 80-120 | 130-160 | 160-200 |
| V,OH | 30-50 | 50-70 | 75-105 | 100-140 | — | |
Notice:
1. The rod should be baked at 300°C -350°C for 1 hours before use.
2. The surfaces to be welded must be cleaned away impurities of oil contamination, rust, moisture and so on.
3. When welding hardenable steel smaller current should be applied and for the big and thick weldment it should be preheated to 150°C before welding.