Product Description
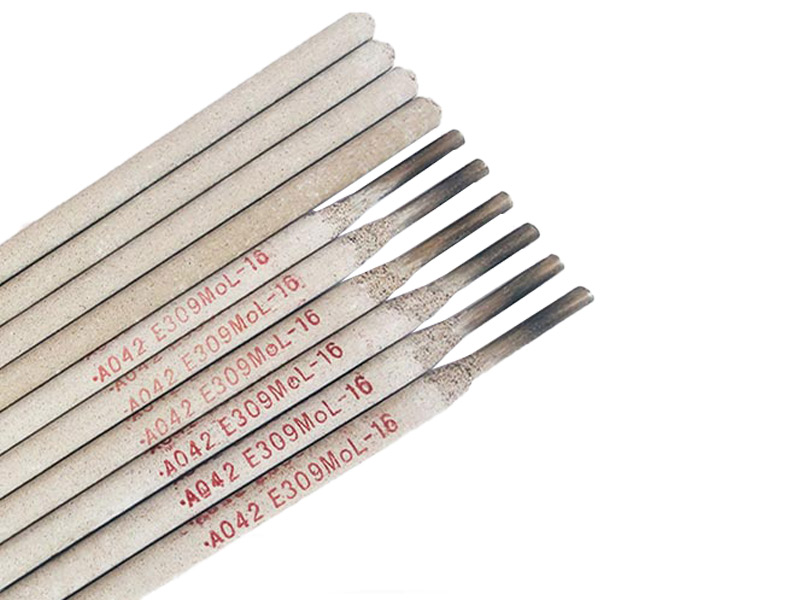
Stainless Steel Electrode E309MoL-16
AWS A5.4 E309LMo-16
IS0 3581-B-ES309LMo-16
BS EN 1600-E23122LR32
CSA W48 E309LMo-16
JIS Z3221 E309LMo-16
GB/T 983 E309LMo-16
Type of Covering: Lime-titania
Welding Position: F,H,HF,OH,V
Type of Current: AC or DCEP
Features & Applications
E309LMo-16 is suitable for welding corresponding extra-low carbon stainless steel structures and dissimilar steels, e.g. ammonia or urea converters.
Chemical Composition of Deposited Metal(%)
| C | Mn | Si | Cr | Ni | Mo | Cu | S | P | |
| Standard | ≤0.04 | 0.50-2.50 | ≤0.09 | 22.0-25.0 | 12.0-14.0 | 2.00-3.00 | ≤0.75 | ≤0.03 | ≤0.04 |
| Typical | 0.025 | 0.96 | 0.65 | 23.24 | 13.35 | 2.45 | 0.18 | 0.012 | 0.024 |
Mechanical Properties of Deposited Metal(AW)
| Tensile Strength Rm(Mpa) | Elongation A4(%) | |
| Standard | ≥550 | ≥30 |
| Typical | 653 | 37 |
Size,Piece & Recommended Current(AC or DC⁺)
| Size(mm) | 2.5×300 | 3.2×350 | 4.0×400 | 5.0×400 | |
| Piece(5kg) | ≈255 | ≈118 | ≈71 | ≈45 | |
| Current(A) | F,H | 50-85 | 80-110 | 130-160 | 160-220 |
| V,OH | 40-60 | 75-105 | 105-135 | — | |
Notice:
1. The rod should be baked at 300°C -350°C for 1 hours before use.
2. The surfaces to be welded must be cleaned away impurities of oil contamination, rust, moisture and so on.
3. Smaller current& short arc are recommended in welding and weave beads no wider than 2.5 times of the diameter of the core rod is better.