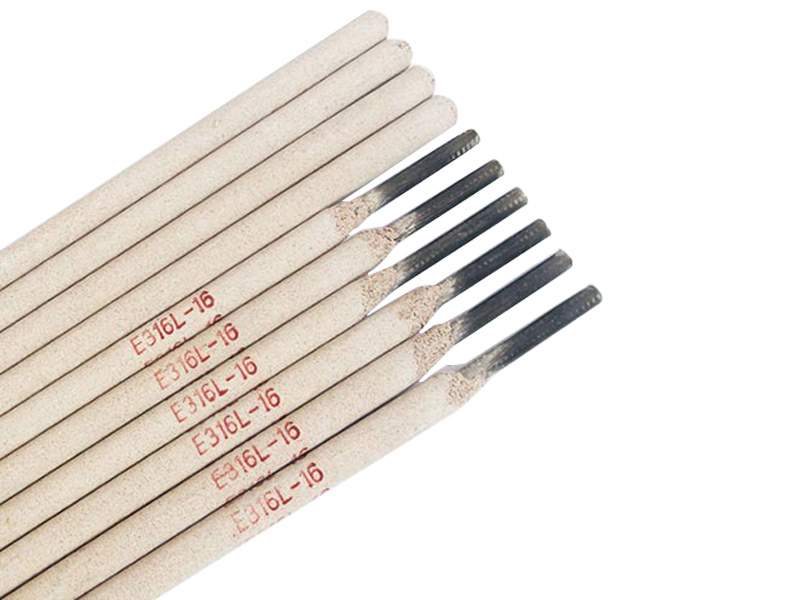
Stainless Steel Electrode E316L-16
AWS A5.4 E316L-16
IS0 3581-B-ES316L-16
BS EN 1600-E19123LR32
CSA W48-01 E316L-16
JIS Z3221 D316L-16
GB/T 983 E316L-16
Type of Covering: Lime-titania
Welding Position: F,H,HF,OH,V
Type of Current: AC or DCEP
Features & Applications
E316L-16 is suitable for welding facilities of synthetic fibre or urea, as well as for similar stainless steel structures. Also it could be used for welding structures made by category of chromium stainless steels that could not be PWHT or for welding dissimilar steels and ply steels. The weld metal has good performance of resistance to corrosion, heat and crack defect.
Chemical Composition of Deposited Metal(%)
| C | Mn | Si | Cr | Ni | Mo | Cu | S | P | |
| Standard | ≤0.04 | 0.50-2.50 | ≤1.00 | 17.0-20.0 | 11.1-14.0 | 2.0-3.0 | ≤0.75 | ≤0.03 | ≤0.04 |
| Typical | 0.030 | 0.85 | 0.62 | 19 | 11.86 | 2.50 | 0.16 | 0.012 | 0.028 |
Mechanical Properties of Deposited Metal(AW)
| Tensile Strength Rm(Mpa) | Elongation A4(%) | |
| Standard | ≥490 | ≥30 |
| Typical | 575 | 44 |
Size,Piece & Recommended Current(AC or DC⁺)
| Size(mm) | 2.0×300 | 2.5×300 | 3.2×350 | 4.0×400 | 5.0×400 | |
| Piece(5kg) | ≈400 | ≈300 | ≈132 | ≈77 | ≈53 | |
| Current(A) | F,H | 30-50 | 60-85 | 85-120 | 115-160 | 160-200 |
| V,OH | 30-45 | 50-70 | 75-105 | 95-140 | — | |
Notice:
1. The rod should be baked at 300°C -350°C for 1hours before use.
2. The surfaces to be welded must be cleaned away impurities of oil contamination, rust, moisture and so on.
3. Smaller current & short arc are recommended in welding and weave beads no wider than 2.5 times of the diameter of the core rod is better