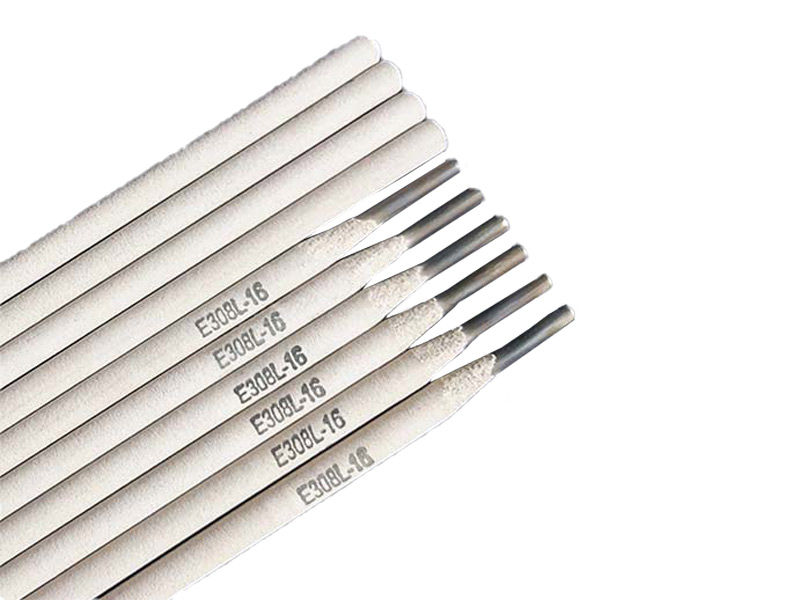
Stainless Steel Electrode E308L-16
AWS A5.4 E308L-16
IS0 3581-B-ES308L-16
BS EN 1600-E 19 9L R 32
CSA W48-01 E308L-16
JIS Z3221 D308L-16
GB/T 983 E308L-16
Type of Covering: Lime-titania
Welding Position: F,H,HF,OH,V
Type of Current: AC or DCEP
Features & Applications
E308L-16 is used for welding stainless steel structures that fabricated by 022Cr19Ni10 or 06Cr18Ni11Ti (e.g.304L or 308L) stainless steel, which work temperature lower than 300°C, such as facilities of synthetic fibre,fertilizer, petrochemical equipment and so on. The weld metal has good resistance to intercrystalline corrosion.
Chemical Composition of Deposited Metal(%)
| C | Mn | Si | Cr | Ni | Mo | Cu | S | P | |
| Standard | ≤0.04 | 0.50-2.50 | ≤1.00 | 18.0-21.0 | 9.0-11.0 | ≤0.75 | ≤0.75 | ≤0.03 | ≤0.04 |
| Typical | 0.029 | 0.86 | 0.63 | 19.8 | 9.60 | 0.078 | 0.10 | 0.012 | 0.024 |
Mechanical Properties of Deposited Metal(AW)
| Tensile Strength Rm(Mpa) | Elongation A4(%) | |
| Standard | ≥520 | ≥35 |
| Typical | 575 | 46 |
Size,Piece & Recommended Current(AC or DC⁺)
| Size(mm) | 2.0×300 | 2.5×300 | 3.2×350 | 4.0×400 | 5.0×400 | |
| Piece(5kg) | ≈430 | ≈275 | ≈142 | ≈83 | ≈55 | |
| Current(A) | F,H | 30-50 | 60-85 | 85-120 | 115-160 | 160-200 |
| V.OH | 30-45 | 50-70 | 75-105 | 95-130 | — | |
Notice:
1. The rod should be baked at 300°C -350°C for 1 hours before use.
2. The surfaces to be welded must be cleaned away impurities of oil contamination, rust, moisture and so on
3. Smaller curent & short arc are recommended in welding and weave beads no wider than 2.5 times of the diameter of the core rod is better.